How to Qualify a Terminal Block Supplier for OEM Production
Qualify the exact product, factory, configuration, and controlled production process—not a logo or a low quote. Use non-negotiable gates for application fit, product evidence, certification scope, production-intent samples, traceability, and change control. Compare cost, service, capacity, and lead time only after those gates are closed.
Approve a controlled configuration
The approval unit is not “Supplier A.” It is a defined terminal family and accessory system, from a named site, made by a controlled process, for a stated OEM use and market route.
Product and application fit
Exact SKU, revision, function, conductor data, ratings, drawings, rail interface, accessories, and end-product conditions agree.
Factory and channel identity
Legal entity, manufacturing site, outsourced processes, authorized channel, and commercial chain are known and traceable.
Current conformity evidence
Official records match the model, category, ratings, status, marking, target market, and conditions of use.
Production-intent validation
Samples, inspection records, deviations, and tests link to the proposed tools, materials, site, process, and packaging.
Process and quality control
Material, tooling, measurement, inspection, rework, nonconformance, CAPA, and release controls are demonstrated.
Traceability and change control
Lots, packs, records, PCNs, deviations, EOL events, alternates, and requalification decisions are contractually controlled.
A supplier with an excellent cost, capacity, or service score is still not qualified when the exact product is unidentified, certification scope is unresolved, the production site is unknown, or change notification is not controlled.
Start with the OEM failure risk, not the supplier questionnaire
A low-energy signal terminal, a protective-earth block, a fuse terminal, and a high-current feeder should not follow the same evidence depth. Define the application before requesting a sample.
Define duty and failure consequence
Record equipment type, circuit role, maintenance model, expected life, customer requirements, and the consequence of an open, short, overheating, miswire, or loss of PE continuity.
Classify the exact family
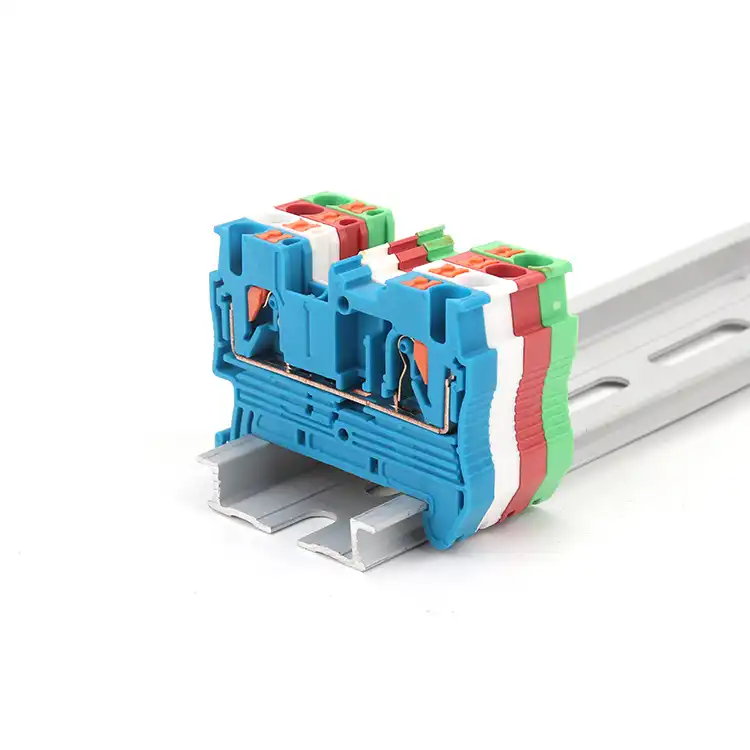
Feed-through, PE/PEN, fuse, disconnect/test, component, distribution, PCB, pluggable, multi-level, shield, or another declared function.
Map conductor and accessories
Conductor material/class, ferrules, entries, rail, bridges, end plates, separators, markers, test plugs, orientation, and enclosure fit.
State electrical and environmental limits
Current, voltage, thermal context, fault duty, vibration, shock, corrosion, chemical exposure, pollution, ingress, and service access.
Identify approval obligations
Destination, end-product standard, component category, customer specification, required declarations, markings, documentation, and transition rules.
Useful next step: establish known requirements with the terminal-block selection guide before requesting a supplier comparison.
Use hard qualification gates before a weighted scorecard
Gates decide whether a candidate may enter the approved comparison. A scorecard then compares candidates that are already technically acceptable.
| Decision area | Hard-gate evidence | Stop condition | Score only after pass |
|---|---|---|---|
| Exact product | Part-numbered data, drawing, revision, function, conductor range, ratings, accessories, and application review. | Only a family brochure, near-match, undocumented alternate, or incompatible accessory. | Engineering response, data maturity, customization support, and catalogue breadth. |
| Conformity route | Official record, category/scheme, named models, ratings, status, marking, use conditions, and end-product assessment. | Logo or screenshot only; identity mismatch; non-current status; no coverage for the SKU or use. | Speed and completeness of compliance support, document access, and market coverage. |
| Factory and process | Named site, QMS scope, process map, controlled materials/tools, inspection, nonconformance, and release records. | Unknown site, undisclosed outsourcing, uncontrolled rework, or records that cannot link to production. | Capacity, flexibility, automation, responsiveness, and improvement maturity. |
| Production validation | Production-intent samples, defined acceptance plan, results, deviations, approval authority, and resubmission rules. | Hand-built sample presented as volume evidence, mixed revisions, or failed criteria without controlled disposition. | NPI lead time, sample support, report quality, and ramp readiness. |
| Lifecycle control | Traceability, quality agreement, PCN/EOL, deviation approval, CAPA, contingency, and requalification triggers. | Unilateral substitutions, no notice commitment, no lot containment path, or no controlled lifecycle record. | Delivery, lead-time stability, service, commercial terms, and continuity planning. |
No universal weighting or passing percentage is recommended. Preserve an engineering or compliance veto for unresolved gates.
ISO 9001 is useful—but it does not qualify the terminal block
ISO 9001:2015, including Amendment 1:2024, remains a quality-management-system framework. A verified certificate can show that a named legal entity and site operate a certified system within a stated scope. It supports questions about controlled processes, documented information, competence, internal audit, corrective action, performance evaluation, and improvement.
It does not certify a terminal block, establish a component rating, prove a specific factory line, validate accessories, or approve the customer’s finished product. Match the certificate to the legal entity, address, scope, certification body, accreditation route, and current status. Then audit the process that will make the quoted SKU.
- QMS certificate: management-system evidence within its stated site and scope.
- Product/component certification: evidence for named models, ratings, conditions, and a certification program.
- Test report: results for identified samples, methods, conditions, deviations, and dates.
- Customer approval: acceptance of a defined configuration and submission—not public certification.
Make the approved evidence auditable months later
The qualification file should let engineering, quality, purchasing, receiving, and production reach the same answer about what was approved.
SKU, revision, site, and configuration
Manufacturer, legal entity, factory, order code, revision, color, terminal function, rail interface, accessory system, packaging, drawing, and CAD.
Ratings and application limits
Conductor construction, connection preparation, current, voltage, temperature/derating, dimensions, materials, environment, and function-specific limits.
Official record and conditions
Standard, certification scheme/category, file or certificate number, model coverage, ratings, status, required marking, and Conditions of Acceptability.
Approved accessories and interfaces
Bridges, end plates, separators, markers, rails, end hardware, plugs, test items, fuse/component inserts, spacing, and assembly instructions.
Controlled declarations
Part/revision scope, resin, metal, plating, flame data, RoHS/REACH information, exemptions, declaration date, and update process.
Repeatability and response records
Process flow, control plan, critical features, gauges, traceability, sample approval, deviations, CAPA, PCN/EOL, packaging, and channel authorization.
Do not accept a logo, screenshot, or supplier-hosted PDF as sole proof. Match the legal manufacturer, address, record number, category, exact model, standard/edition route, ratings, conditions, status, and marking in the issuing body’s official database. Database presence alone does not make unmarked or mismatched stock certified.
A standard, certificate, test report, and CE mark answer different questions
Qualification fails when procurement treats unlike evidence as interchangeable.
| Evidence | What it can support | What it does not prove |
|---|---|---|
| IEC or other standard | Published requirements, classifications, tests, and scope for the relevant product/function. | A standard does not certify a product, factory, supplier, or finished OEM assembly. |
| QMS certificate | A certified management system for the stated legal entity, site, and scope. | Exact SKU performance, production output, product certification, or customer application fit. |
| Component certification | Named models, ratings, use conditions, marking, and program status within the stated category or scheme. | Automatic acceptance of every variant, accessory, enclosure, conductor, or finished product. |
| ISO/IEC 17025 test report | Competent testing where the laboratory’s accredited scope covers the relevant method, with traceable sample and result data. | Product approval, supplier approval, or coverage beyond the identified sample, method, and conditions. |
| CE marking/declaration | The manufacturer’s declaration that applicable EU harmonization requirements are addressed for the product in scope. | EU authority approval or a universal third-party product certificate. |
| PPAP or FAI submission | Customer review of a defined production configuration, run, first article, and evidence package when contractually required. | Public certification, long-term capability proof, or a guarantee for future lots. |
Use the edition required by the end-product route and certification transition rules. A record may remain valid during an authorized transition; do not declare it invalid merely because a newer edition exists.
Audit the real production process, not only the meeting room
ISO 19011:2026 provides management-system audit guidance. Your OEM criteria must still follow the actual terminal technology, outsourced steps, application risk, and evidence gaps.
Who actually makes the part?
Confirm legal entity, site, production line, subcontractors, plating/molding sources, authorized channels, incoming identity, and lot segregation.
How is variation controlled?
Review resin/metal/plating lots, molds, tools, springs, screws, process parameters, work instructions, first-off checks, and reaction plans.
Can results be trusted?
Check critical characteristics, method suitability, gauge identification, calibration status, measurement records, competence, and out-of-tolerance response.
What prevents an escape?
Review in-process and final inspection, nonconforming segregation, rework authorization, lot release, pack labels, quantity control, and shipment traceability.
How are problems contained?
Test containment speed, affected-lot identification, root-cause evidence, corrective action, effectiveness verification, customer communication, and recurrence review.
Who approves a difference?
Inspect PCN, deviation, alternate material/tool/site, label, certificate, sub-supplier, and lifecycle workflows before implementation.
Can one shipment be reconstructed?
Trace from order and carton back to part revision, lot, material/process records, inspection, deviations, release, and responsible site.
Can the approved source keep supplying?
Review realistic capacity evidence, bottlenecks, maintenance, long-lead inputs, inventory policy, recovery plans, EOL notice, and approved alternate strategy.
Audit depth can be document-based, remote, on-site, or combined. Choose it from risk and evidence—not from a universal duration or checklist score.
Derive them from the approved drawing, certification conditions, assembly interface, failure analysis, and OEM use. A universal Cpk threshold is not appropriate for every feature, and 100 percent inspection does not guarantee zero defects or replace process control.
Validate the configuration that will actually enter volume production
Samples should link to the proposed manufacturing site, production tools, materials, process, marking, revision, accessories, and pack format. Define the acceptance plan before testing: identity, lot, quantity, methods, conditions, equipment, pass/fail criteria, deviations, retained records, approval authority, and resubmission triggers.
Use the customer-mandated approval route. AIAG PPAP is an automotive production-part approval method; SAE AS9102C defines aerospace first article inspection documentation. A general industrial OEM should use its own production-part or first-article plan unless the contract invokes PPAP, AS9102C, or another sector method.
- Screening sample: useful for early fit and feasibility, but not automatically production evidence.
- Production-intent sample: linked to the intended site, tooling, materials, process, and controlled revision.
- Golden sample: a controlled visual/physical reference only for characteristics it can actually represent.
- PPAP/FAI acceptance: customer approval of a defined package, not product certification or future-lot guarantee.
Turn one good sample into a controlled production system
Approval is maintained through traceability, monitoring, controlled change, containment, and evidence-based requalification.
Freeze the approved baseline
Record SKU, revision, site, materials, tooling/process, accessories, labels, pack, certificates, declarations, drawings, samples, deviations, and approval authority.
Connect every shipment
Define traceability from purchase order and carton to product lot, revision, source, material/process records, inspection, release, and any deviation.
Monitor real performance
Trend lot rejects, escapes, complaints, CAPA closure/effectiveness, audit findings, PCN compliance, on-time delivery, lead-time stability, and field returns by family and site.
Control change and disruption
Assess material, tool, process, site, sub-supplier, marking, packaging, approval, capacity, PCN, and EOL impacts before release.
A change requires documented assessment. Requalify the affected evidence and functions unless the quality agreement, customer requirement, or end-product certification route requires a broader or full requalification.
Keep approved identity connected through shipment
Traceability granularity is a risk decision, but it should be clear enough to contain a defect without treating all historical production as suspect. Define the meaning of lot, pack, date code, production line, material batch, inspection record, and shipment reference before launch.
Receiving evidence should let the OEM verify manufacturer, SKU, revision, quantity, source/channel, required markings, lot/pack identity, packaging condition, customer label, and open deviation status. Authenticity controls should prioritize authorized supply routes and issuer-verifiable records—not packaging appearance alone.
- Backward trace: shipment to lot, revision, site, material/process records, inspection, and release.
- Forward trace: affected lot to cartons, shipments, customers, stock, work orders, and finished OEM units where required.
- Containment: defined authority, communication timing, shipment hold, suspect-stock control, and evidence of effectiveness.
Use a scorecard to compare qualified candidates
Weights should reflect program risk. Do not publish one “correct” percentage or let a total score overrule an unresolved hard gate.
Configuration and data maturity
Part-specific drawings, ratings, limits, accessories, CAD, revisions, approval records, and engineering response quality.
Control and repeatability
Audit findings, critical-feature control, measurement validity, defect history, rework discipline, CAPA closure, and effectiveness.
Sample-to-production linkage
Production-intent evidence, validation completion, deviations, submission quality, tooling/process readiness, and launch response.
Current, verifiable records
Certificate/database match, use-condition support, material declarations, update discipline, and end-market documentation.
Capacity, lifecycle, and recovery
Lead-time performance, bottleneck evidence, maintenance, inventory, PCN/EOL behavior, alternate readiness, and recovery planning.
Total program fit
Landed cost, MOQ, pack, payment/contract terms, documentation speed, sample support, problem response, and OEM coordination.
Red flags that should pause volume approval
A fast stop is cheaper than a field containment, certification gap, or uncontrolled redesign.
Request evidence for the exact OEM production requirement
Send SENTOP the application, BOM or drawing, target markets, volume, sample plan, documentation needs, packaging, labeling, and change-control expectations. SENTOP can coordinate model matching, samples, documentation, OEM packaging, and supply evidence; the customer remains responsible for supplier approval and finished-product compliance.
Continue from supplier qualification to a controlled sourcing package
Terminal block supplier qualification questions
Is ISO 9001 certification enough to approve a terminal block supplier?
No. ISO 9001 is useful quality-management-system evidence, but it does not certify the terminal block or prove the exact factory, product variant, accessory system, certification coverage, sample performance, or end-product suitability. Verify the certificate scope and site, then qualify the actual production configuration.
What is the first hard gate for a new terminal block supplier?
Start with exact product identity and intended application fit. Require the ordering code, revision, function, conductor and connection data, ratings, drawings, rail and accessory compatibility, manufacturing site, target markets, and production configuration.
Does a UL mark make a terminal block automatically acceptable?
No. Verify the official file or certification record, category, legal manufacturer, exact model, ratings, status, required marking, and Conditions of Acceptability. Then confirm that the OEM enclosure, wiring, conductor, temperature, accessories, and end-product route satisfy those conditions.
Should every terminal block supplier receive an on-site audit?
Not necessarily. Use a risk-based approach. A standard, dual-sourced signal terminal may begin with document review and production samples, while PE, fuse, high-current, regulated, harsh-environment, single-source, or safety-related uses can justify deeper remote or on-site process evidence.
Are PPAP or FAI always required for terminal blocks?
No. Use the approval route required by the customer, contract, and industry. AIAG PPAP is an automotive method and SAE AS9102C defines aerospace first article inspection documentation. A general industrial OEM can use its own production-part or first-article plan.
Which samples should be used for qualification?
Use samples traceable to the proposed production site, tools, materials, process, marking, revision, accessories, and packaging. A prototype or sales sample can support early screening, but it should not be the sole volume-release basis when the final production configuration differs.
Is AQL sampling enough to prove terminal block quality?
No. ISO 2859-1 acceptance sampling can support an OEM-defined lot decision, but it is not proof of safety, reliability, process capability, or end-product compliance. Critical characteristics may require validated controls, enhanced sampling, independent evidence, or full verification.
What documents should the supplier provide?
Request part-numbered data and drawings, connection and rating information, certification records and use conditions, accessory compatibility, material declarations, manufacturing-site and QMS evidence, production-intent approval records, packaging and traceability information, and PCN, EOL, deviation, and CAPA terms.
How often should a terminal block supplier be requalified?
Use a planned review cadence plus event-based triggers. Requalification or intensified review can follow a product, material, process, site, approval, or supplier change; recurring defects; a field issue; EOL; prolonged inactivity; or a material change in the OEM application.
Can a lower-cost terminal block be approved because it has the same dimensions?
No. Dimensions alone do not prove function, conductor acceptance, ratings, thermal behavior, rail and accessory compatibility, materials, certification scope, manufacturing controls, change process, or finished-product effects. Treat the near-match as a new candidate.
Standards, certification, audit, and production sources
Confirm the current edition and transition rules that apply to the actual market, customer, and end-product route at the time of release.
- IEC 60947-7-1:2025. Terminal blocks for copper conductors.
- IEC 60947-7-2. Protective-conductor terminal blocks.
- ISO 9001:2015 with Amd 1:2024. Quality management systems requirements.
- ISO 19011:2026. Guidelines for auditing management systems.
- ISO 2859-1:2026. Acceptance sampling by attributes.
- ISO 10012:2026. Quality management requirements for measurement processes and equipment.
- ISO/IEC 17025:2017. Competence of testing and calibration laboratories.
- ISO certificate verification. ISO explanation of certification and checking a certificate.
- UL Component Recognition. Recognition and Conditions of Acceptability.
- UL Product iQ. Official product sourcing and certification database information.
- UL 508A Supplement SA. Current controlled component-requirements landing page.
- IEC FAQ. Standards publication versus testing and certification boundary.
- European Commission. CE marking responsibility and meaning.
- European Commission. RoHS Directive context.
- ECHA. Candidate List substances in articles and supply-chain communication.
- IEC 82474-1:2025. Material declaration for products and the electrical industry.
- AIAG PPAP. Automotive Production Part Approval Process manual.
- SAE AS9102C. Aerospace first article inspection requirement.
- Phoenix Contact. Terminal-block quality-test evidence examples.
- Schneider Electric. Terminal-block product change notification example.
Qualify the exact terminal system, then keep the approved evidence connected
Send the application, target market, BOM, forecast, sample plan, documentation requirements, packaging, and change-control expectations for a model and supply review.